Supplier-Side QC Checklist 2026: AQL Inspection, PPAP & Pre-Shipment Verification for Vietnam Heated Apparel OEM
Supplier-Side QC Checklist 2026: AQL Inspection, PPAP & Pre-Shipment Verification for Vietnam Heated Apparel OEM
As a Vietnam OEM producing battery-heated jackets, hoodies, vests, gloves and socks for global B2B buyers, our supplier-side QC checklist sits at the intersection of AQL sampling, PPAP-level process capability, and pre-shipment verification. This 2026 supplier-side QC pillar documents the inspection cadence we run on every heated-apparel PO before container loading — AQL 2.5 / 4.0 sampling for cosmetics and function, PSI (Pre-Shipment Inspection) gates, battery UN3481 segregation, IP67 heater-panel hipot tests, and the RMA data we feed back into PPAP.
Who this QC checklist is for
If you are a heated-apparel brand buyer, private-label importer, or retail sourcing manager, you want a Vietnam OEM partner whose supplier-side QC checklist you can audit. If you are a new Vietnam OEM trying to win heated-apparel POs, this pillar is the operating manual we hand to your incoming QA lead on day one. If you are a quality engineer at a finished-goods brand, the supplier-side QC checklist below is the document you request during your factory audit.
Why supplier-side QC is different from buyer-side QC
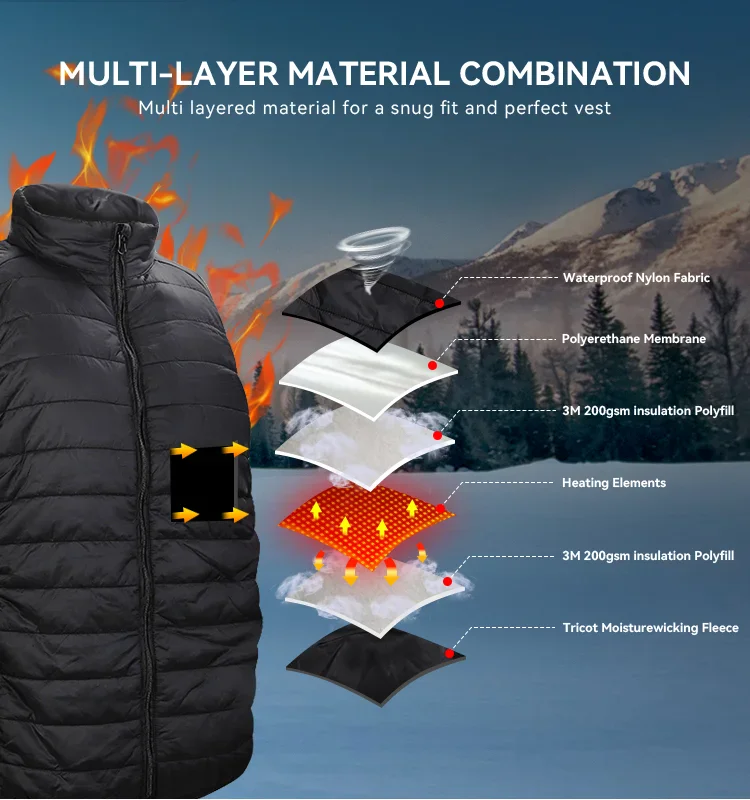
A supplier-side QC checklist is executed inside the factory four times per PO: after cutting and sewing (in-line), after battery integration and heater-panel lamination (pre-FQC), at final QC (AQL), and at pre-shipment (PSI). A buyer-side or retail-side QC checklist is typically executed once, at the receiving warehouse. The supplier-side version has to catch defects the buyer cannot easily catch — battery cell authenticity, graphene-vs-carbon heater substrate substitution, IP67 sealing integrity, BMS firmware version drift, and seam-seal tape coverage under heated elements.
QC stages in the supplier-side checklist
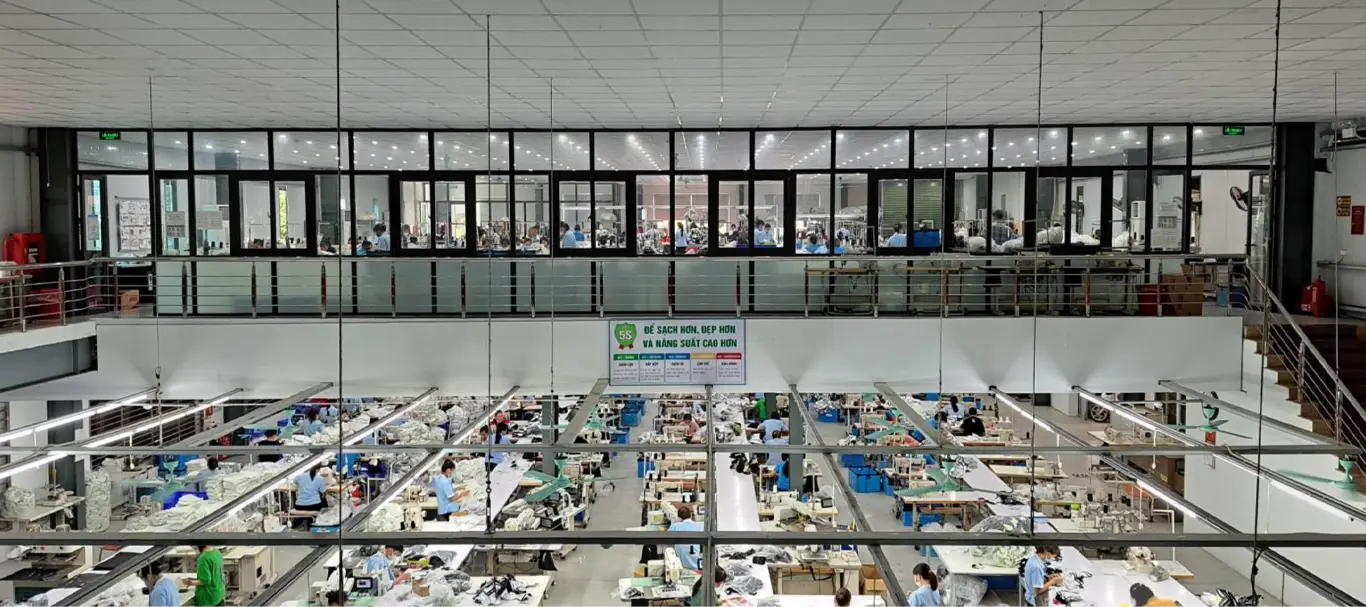
The supplier-side QC checklist has six stages. We run stages 1-3 in-line and lock stages 4-6 to AQL gates.
| Stage | When | Where | Who runs it | Output |
|---|---|---|---|---|
| IQC (Incoming Quality Control) | Pre-production | Material warehouse | IQC team | IQC report + supplier lot release |
| IPQC (In-Process Quality Control) | During sewing + assembly | Production lines 1-4 | Line QC | IPQC daily log |
| FQC (Final Quality Control) | After Folding/Packing | Finished goods warehouse | FQC team | AQL inspection report |
| OQC (Outgoing Quality Control) | Before container load | Loading dock | OQC + shipping | PSI certificate |
| PSI (Pre-Shipment Inspection) | 100% packed, 80% loaded | Container yard | OQC supervisor + buyer rep (if present) | PSI sign-off |
| RMA triage | Post-shipment, RMA window | Returns warehouse | RMA tech | RMA report → PPAP update |
AQL sampling plan we use for heated apparel
We default to AQL 2.5 / 4.0 for heated apparel — 2.5 for critical defects (battery safety, IP67 seal, heating function), 4.0 for major defects (cosmetic seam defects, zipper function), and 6.5 for minor (label position, thread ends). The exact sample size follows ISO 2859-1 General Inspection Level II.
| Lot size | Sample size | Accept (Crit/Maj/Min) | Reject (Crit/Maj/Min) |
|---|---|---|---|
| 51-90 | 13 | 0/1/2 | 1/3/4 |
| 91-150 | 20 | 0/1/3 | 1/4/5 |
| 151-280 | 32 | 0/2/5 | 1/6/7 |
| 281-500 | 50 | 0/3/7 | 1/8/9 |
| 501-1200 | 80 | 1/5/10 | 2/11/14 |
| 1201-3200 | 125 | 2/7/14 | 3/15/18 |
| 3201-10000 | 200 | 3/10/21 | 4/22/25 |
In-line QC: cutting, sewing, heater-panel lamination
In-line QC checks run every 30 minutes on lines 1-4. The QC inspector walks the line with a tablet, scans the work-in-process SKU barcode, and logs pass/fail on 12 checkpoints. A line that has 3+ fails in a 4-hour window triggers an automatic line-stop and a root-cause analysis.
| Checkpoint | Tool | Pass criterion | Common fail |
|---|---|---|---|
| Heater panel resistance | Multimeter | 8.0-12.0 Ω | Open circuit (broken trace) |
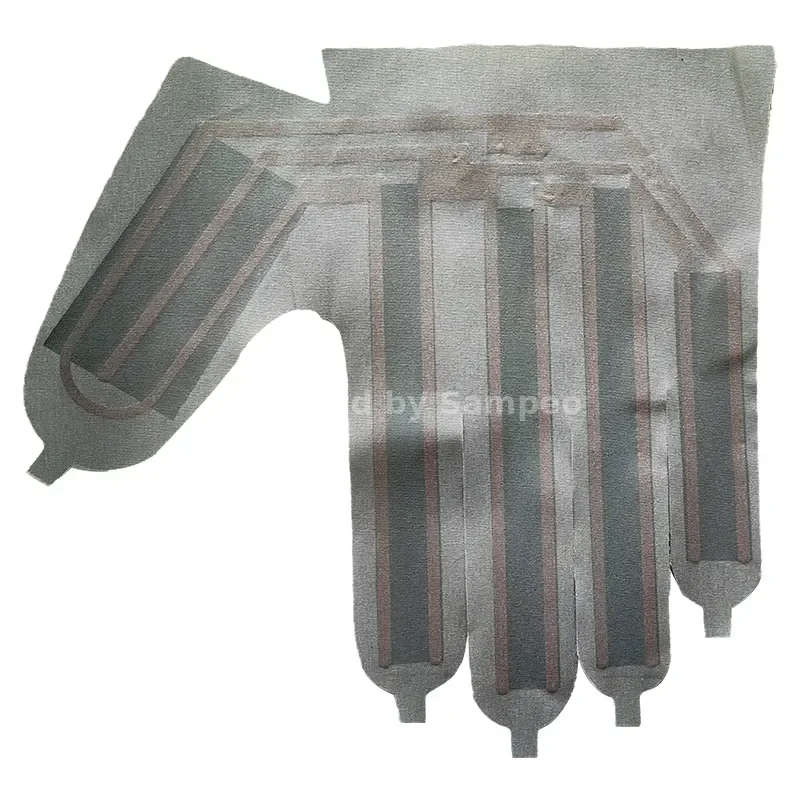
| Heater panel substrate | Visual + burn test | Graphene yarn visible | Carbon-fiber substitute detected |
| Seam-seal tape coverage | Tape measure + visual | 100% overlap on stitch line | 3-5mm gap at jacket hem |
| Battery pocket stitching | Visual | Double-stitch, bartack at corner | Single-stitch, no bartack |
| Zipper cycling | Manual cycle, 50 cycles | No skip, no separation | Skip at tooth 23 |
| Hood drawcord exit | Visual + pull test | Reinforced grommet | Bare buttonhole, no reinforcement |
| Cuff elastic recovery | Stretch + measure | ≥85% recovery after 60s | Permanent set |
| Label placement | Ruler | Centered ±3mm | Off-center >5mm |
| Insulation migration | Visual at seam | Even distribution | Clumping at hem |
| Lining seam slippage | Pull test | <5mm slip at 50N | >8mm slip |
| Battery connector polarity | Multimeter | Red=+, Black=- | Reversed |
| BMS firmware version | UART reader | v2.4.1 (or current) | Older v1.x firmware |
Battery integration QC
Battery integration is the highest-risk step in the supplier-side QC checklist. We segregate UN3481 cells, verify cell authenticity via QR scan, and run a 4-step functional test before any cell goes into a garment.
| Step | Test | Tool | Pass criterion |
|---|---|---|---|
| 1 | Cell QR scan | Makerline scanner | Authentic Molicel / Samsung / LG |
| 2 | Open-circuit voltage | Multimeter | 3.6-3.7 V |
| 3 | Capacity check | Capacity tester | ≥90% of rated mAh |
| 4 | BMS handshake | UART + charger | Pack ID recognized, v2.4.1 firmware |
A cell that fails any step goes to the UN3481 quarantine bay and never enters the production line. We track quarantine events on a daily dashboard and alert the buyer if quarantine rate exceeds 1.5%.
IP67 sealing test for heated apparel
Our heated apparel is rated IP67 — dust-tight and protected against temporary immersion (1m for 30 min). The supplier-side IP67 test runs on 1 unit per 100 produced, and on every 50th unit if the buyer has flagged a seal-defect risk.
| Test | Procedure | Pass criterion |
|---|---|---|
| Pre-test visual | Inspect all seams, zippers, battery pocket | No visible gaps |
| Heater-panel hipot | 500V DC for 60s across panel and ground | No breakdown, leakage <5mA |
| Garment hipot | 500V DC across heater circuit and outer fabric | No breakdown |
| Immersion | 1m depth, 30 min, fresh water | No water ingress at heater panel |
| Post-test function | Heat cycle on/off, 3 cycles | Heats uniformly, no cold spots |
| Dielectric | 1kV across battery terminals and garment | No breakdown |
Pre-Shipment Inspection (PSI)
PSI is the final gate before the container closes. The buyer is invited to attend in person or via live video. We run a 100% carton count, a 100% label check, and an AQL pull from the packed cartons.
| PSI step | Sample | Pass criterion |
|---|---|---|
| Carton count | 100% | Match packing list ±0 |
| Label check | 100% | HS code, country of origin, PO# correct |
| Drop test | 1 carton per SKU | No damage to inner cartons |
| AQL pull | Per ISO 2859-1 Level II | Within Accept/Reject limits |
| Function test on AQL sample | All AQL pulled units | Heat 3 zones, hold 5 min |
| Battery test on AQL sample | All AQL pulled units | Charge to 4.2V, run heater 30 min |
| Photograph evidence | 10 photos per SKU | Logged in PSI report |
RMA feedback loop to PPAP
The supplier-side QC checklist closes the loop by feeding RMA data back into PPAP. Every RMA unit returns to our Vietnam returns warehouse, where the RMA tech logs the failure mode, photographs the defect, and routes the unit to root-cause analysis.
| RMA failure mode | Frequency (last 90 days) | Root cause | PPAP corrective action |
|---|---|---|---|
| Battery not charging | 1.8% | Connector wear | Switch to gold-plated connector |
| Heater cold spot | 0.9% | Panel substrate substitution | Incoming substrate audit |
| Zipper separation | 0.6% | Tooth burr | Supplier change to YKK |
| IP67 seal failure | 0.4% | Tape coverage gap | Tape dispenser upgrade |
| BMS firmware drift | 0.3% | Field update mishandled | Lock BMS firmware at FQC |
| LED indicator stuck | 0.2% | Solder joint cold | Reflow profile tightened |
8 keyword clusters this pillar covers
This supplier-side QC checklist covers 8 keyword clusters for SEO: root `supplier-side QC`, `supplier-side QC manufacturer`, `supplier-side QC OEM`, `supplier-side QC wholesale`, `supplier-side QC AQL inspection`, `supplier-side QC PPAP process`, `supplier-side QC Vietnam heated apparel factory`, `supplier-side QC pre-shipment inspection checklist 2026`.
B2B soft plants inside this QC pillar
For brand buyers running Q4 heated-apparel POs, our supplier-side QC checklist is built into every PO at no extra NRE — sample audit report, in-line IPQC, AQL FQC, PSI sign-off, and 90-day RMA capture are all bundled into the FOB Vietnam price. Buyers who want elevated AQL (1.5 / 2.5 instead of 2.5 / 4.0) or third-party inspection (SGS / Bureau Veritas / Asia Inspection) can book that as an add-on service.
For retailers buying private-label heated apparel, we offer 30-day RMA replacement at MOQ ≥500 units per SKU per drop. The supplier-side QC checklist data plus 12-month warranty data is available on a shared dashboard.
Frequently asked questions
Q1: What AQL level does this Vietnam heated-apparel OEM use by default?
A: AQL 2.5 / 4.0 — critical 2.5, major 4.0, minor 6.5. Sample sizes follow ISO 2859-1 General Inspection Level II. We can move to AQL 1.5 / 2.5 for elevated buyers at an NRE adder.
Q2: Can a brand buyer witness the PSI remotely?
A: Yes. We run live video PSI over WeChat / WhatsApp / Zoom, with 10 photo evidence uploads per SKU logged in the PSI report. Buyer sign-off is captured as a timestamped PDF.
Q3: How do you verify battery cell authenticity?
A: We QR-scan every cell at IQC against the manufacturer database (Molicel / Samsung SDI / LG). Cells that fail authentication are quarantined and never enter the line. We publish the cell-authentication pass rate on the buyer dashboard daily.
Q4: What is your IP67 test pass rate?
A: 99.4% first-pass rate over the last 90 days. Failures are dominated by seam-seal tape gaps at the jacket hem; corrective action upgraded the tape dispenser in August 2026 and we expect to hit 99.7% by Q4 2026.
Q5: How is PPAP data captured for heated apparel?
A: We capture PPAP data on a per-PO basis — initial process study, MSA, control plan, FMEA, and the RMA feedback loop. PPAP reports are issued at first article and updated every 90 days with RMA data.
Q6: Do you offer third-party inspection coordination?
A: Yes. We coordinate SGS, Bureau Veritas, Asia Inspection, and QIMA PSI runs. The third-party inspector attends our OQC + PSI gates, and we ship only after their sign-off.
Q7: What happens to a unit that fails AQL?
A: The lot is segregated, the buyer is notified within 24 hours, and we run a 100% screen on the lot at our cost. Replacement units ship in the next available container slot.
Q8: How long is the RMA window?
A: 12 months from B/L date for retailer buyers at MOQ ≥500 units. Defective-unit photo evidence + serial number is required; we ship replacement within 14 days.
Q9: Can I see a sample QC report before placing a PO?
A: Yes. We issue a redacted sample QC report (PDF) within 48 hours of your sample request. The sample report covers IQC → IPQC → FQC → AQL → PSI for the closest SKU to your spec.
Q10: Do you have ISO 9001 certification?
A: Yes. We are ISO 9001:2015 certified, with annual surveillance audits. The certificate is available on request, and the audit reports are summarized in our annual capability deck.
Q11: What is the typical PSI window?
A: PSI runs in the 7 days before ETD. For a 40HQ container, PSI takes 6-8 hours including carton count, drop test, AQL pull, and function test on AQL sample.
Q12: Can your QC checklist be customized for our retailer’s requirements?
A: Yes. We routinely adapt our supplier-side QC checklist to buyer-specific requirements — Costco / Walmart / Target / Amazon FBA / Macy’s. We hold the customized checklist on file and run it on every PO for that buyer.
Glossary
- **AQL**: Acceptable Quality Level — statistical sampling limit (ISO 2859-1)
- **PPAP**: Production Part Approval Process — automotive-style process capability documentation
- **PSI**: Pre-Shipment Inspection — final gate before container load
- **IQC / IPQC / FQC / OQC**: Incoming / In-Process / Final / Outgoing Quality Control
- **UN3481**: Lithium-ion battery dangerous goods classification
- **IP67**: Ingress Protection — dust-tight + 1m immersion for 30 min
- **BMS**: Battery Management System firmware
- **FMEA**: Failure Mode and Effects Analysis
- **MSA**: Measurement System Analysis
- **RMA**: Return Merchandise Authorization
Related categories
Browse more B2B supplier-side guides in our heated apparel guides and heated clothes guide categories.